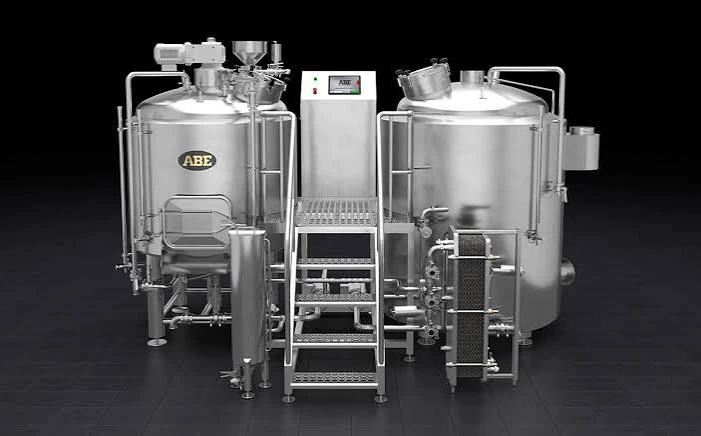
Steam-heated brewhouses depend on condensate leaving jackets and heat exchangers at the right rate. A failed steam trap can waste energy, slow heating, or leave condensate where it reduces heat transfer. Inspection is not simply listening for a hiss. Identify each trap, compare its inlet and outlet behavior under normal load, and have a qualified person confirm the diagnosis before changing the device.
Map the trap to the process
Create a simple drawing showing steam supply, vessel jacket or coil, trap, condensate return, isolation valves, and any strainer. Label each trap with the equipment it serves. A kettle and a hot-water tank may behave differently; comparing them without accounting for load can mislead the technician. Record the steam pressure and operating state permitted by the equipment design, but do not adjust a trap to compensate for a poorly configured system.
Ask operators where they see slow heat-up, water hammer, or inconsistent temperature control. These symptoms help prioritize inspection, yet none proves a particular trap has failed. Water hammer and hot condensate can cause severe injury. Only trained staff should isolate, cool, and service the system under the site’s lockout procedure.
Use more than one observation
Check for leaking connections, plugged strainers, unusual vibration, and evidence of condensate backing up. Temperature, sound, and ultrasonic checks may help, but interpret them against the trap type and current load. A trap that passes steam continuously may heat the return line; a blocked trap may leave the jacket underperforming. A quiet trap is not automatically healthy.
If the brewhouse has been modified, verify that trap capacity and orientation still match the application. An undersized or wrongly oriented replacement can reproduce the same symptoms. Request the trap manufacturer’s service guidance and confirm material compatibility with the steam and condensate system.
Close the loop after repair
Record the trap location, fault, replacement part, and operating condition after service. Compare kettle or hot-water heat-up behavior with the pre-repair baseline. If the trap repeatedly fails, investigate water quality, strainer maintenance, and upstream control rather than treating replacement as routine.
When specifying brewery equipment or planning a new craft brewhouse, include condensate routing and accessible trap locations in the design review. An accessible, documented trap is easier to maintain safely and less likely to become an invisible source of poor process control.
Make the inspection route repeatable
Number the traps on a site drawing and inspect them in the same order. Note whether the served equipment was heating, holding, or idle. A temperature or sound reading taken while a jacket is cold cannot be compared directly with one taken during vigorous boiling. Record observations beside the operating state, then repeat suspect measurements when the load returns. A handheld infrared reading on an uninsulated pipe may help locate a change, but emissivity, insulation, and distance can mislead; it should not be the only basis for replacing a trap.
If several traps fail together, investigate steam and condensate conditions upstream. A system problem can damage replacements quickly. Check whether operators have been opening bypass valves to keep the brewhouse running; a bypass can hide a failed trap and waste steam continuously.
Include access in the maintenance plan
Reserve space for isolation, removal, and safe cooling. If a trap sits behind a hot vessel or above a walkway, servicing may be deferred until it fails badly. Include strainers and test points in the drawing, label them, and keep spares identified by type and capacity. After a repair, verify heat-up time and condensate return behavior over more than one brew. A successful repair should restore the process result, not merely eliminate an unusual noise.
Put the findings into a maintenance decision
An inspection sheet should identify the trap, process load, observations, likely failure mode, and next action. Separate “monitor,” “service at the next shutdown,” and “isolate now” decisions using the brewery’s safety criteria. A suspect trap on a critical kettle may justify a planned downtime window, while a noisy but functioning trap may need another measurement under steady load. Have a qualified technician review uncertain results. Do not let an operator remove insulation or touch a hot line merely to satisfy a checklist.
When a trap is replaced, retain the old part long enough to inspect it. A blocked strainer, damaged seat, or wrong-size part can point to a wider system issue. Compare the new part with the original specification and note any intentional change. If heat-up improves, record the new time and steam usage if measured. This converts a repair into a useful baseline for the next inspection.
Watch the condensate return
Condensate is not waste by default; many plants recover it. Check whether the return line is sized, supported, and routed to avoid backpressure that interferes with trap operation. A trap may appear faulty when the return system is restricted. Observe whether several pieces of equipment slow down at once. That pattern suggests a common return problem rather than three independent trap failures.
Water hammer deserves prompt investigation because it can damage equipment and injure workers. Record when it occurs: start-up, valve closure, or a particular heat-up step. Do not suppress the noise with an unapproved bypass. The steam-system designer can use that timing to inspect drainage, control valves, and start-up practice.
Specify for the next brewhouse change
If the brewery adds a vessel or changes kettle duty, review steam demand and condensate handling together. The existing trap schedule may no longer fit. Ask for a piping and instrumentation drawing with accessible isolation, strainers, traps, test points, and return connections. A new vessel’s advertised heating rate is only achievable when the steam and condensate system supports it. Documenting the whole path makes future troubleshooting much less dependent on the one technician who remembers how the piping was installed.
An example of a useful work order
Suppose the kettle takes longer to reach boil and the condensate return line is unusually hot. A useful work order records the kettle state, steam pressure, trap ID, return temperature observation, and whether a bypass valve was open. It asks a qualified technician to inspect the trap and return path during a planned safe window. It does not simply say “replace noisy trap.” After service, the brewer records the next comparable heat-up time. This closes the loop between maintenance activity and process performance.
If the new trap does not restore the baseline, the work order should remain open while the team checks the control valve, jacket, and return backpressure. The original symptom may have involved more than one component. Retaining the measurements prevents a cycle of repeated part swaps without diagnosis.
Robert Hayes is an ESL educator and curriculum developer with over nine years of experience teaching English to beginners and intermediate learners across multiple countries ( Biography ).